
Traceable materials for GCC manufacturing
EN 10204 3.1 Material Certs for Machined Components in the GCC
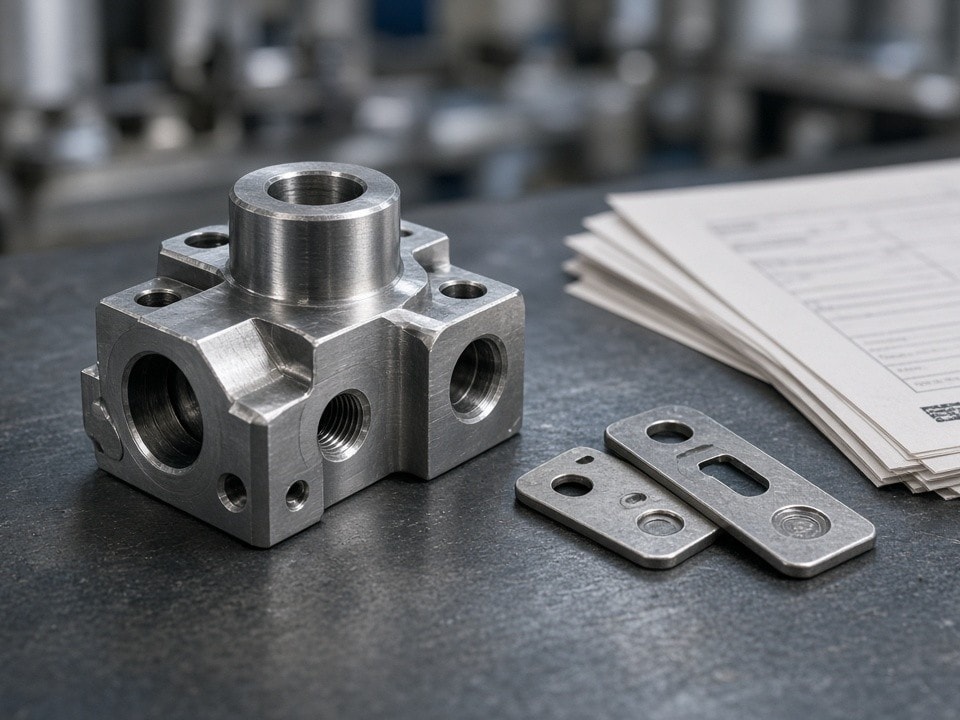
PartsMake supplies finished mechanical parts with EN 10204 3.1 certificates issued against each material heat lot. Trace every component back to its original steel mill and furnace number, with the test results regional EPC contractors and operators need.
Standard supply is EN 10204 3.1. Where a project specification calls for it, an EN 10204 3.2 inspection route can be scoped with your enquiry.
Heat-lot
Traceability to the original melt
10–18 days
For eligible stocked-feedstock parts up to 400 mm cube
1 working day
Quote response with stock and certificate details
Certificate scope
The material record travels with the part
Each EN 10204 3.1 certificate is issued by the material producer and verified by an independent inspector. It connects the finished component to the raw bar or plate and the furnace batch number marked on the material.
A clear traceability chain
- 01Original steel mill and furnace number recorded against the heat lot.
- 02Raw bar or plate identification links the stock to its certificate.
- 03Scanned mill certificates are attached to the final inspection package before dispatch.
Chemical analysis
Composition from the melt
Complete chemical composition results from optical emission spectroscopy, recorded against the certified material heat.
Mechanical testing
Strength and ductility results
Tensile strength, yield strength and elongation are listed for the material batch.
Impact performance
Charpy V-notch values at the specified test temperature
The certificate records the impact-test temperature and absorbed energy values, supporting review against the project’s material requirements.
Manufacturing capability
Certified alloys, matched to the process
Select a capability to review work envelopes, tolerances, common alloys and typical deliverables. Mill certificates are scanned into the final inspection package before dispatch.
| Process | Max envelope | Tolerance | Typical alloys with 3.1 certs | Common GCC parts |
|---|---|---|---|---|
| 5-Axis Milling | 1200 × 1000 × 800 mm | ±0.005 mm | Inconel 718, Super Duplex 2507, Ti-6Al-4V | Pump impellers, valve bodies |
| Mill-Turn 9-Axis | Ø420 × 1050 mm | ±0.005 mm | 17-4PH, Hastelloy C276, Monel 400 | High-pressure manifolds, wellhead spools |
| Heavy Turning | Ø850 × 2200 mm | ±0.008 mm | AISI 4140, 316L, Inconel 625 | Long mandrels, drill collars |
| Gantry Milling | 3500 × 2200 × 1000 mm | ±0.020 mm | Structural carbon steel, SS316 | Skid frames, tube sheets |
GCC project fit
Documentation that supports real procurement needs
Align the material grade, manufacturing route and inspection records with the component’s operating environment and project documentation requirements.
Flow control · Dammam & Jubail
Tier-2 contractors need replacement valve trims in Inconel 718 or Super Duplex 2507 within three weeks. 5-axis capacity and pre-certified stock can help avoid the 24-week OEM wait while supplying the required 3.1 data book.
Skid packages · JAFZA & Yanbu
Small batches of Super Duplex manifolds and laser-slotted intake baskets ship with the plate certificate, PMI report and CMM log attached.
Data-centre cooling
Copper cold plates and busbars can be supplied with full chemical and mechanical traceability for high-temperature service. Vacuum-brazed assemblies retain the same 3.1 documentation on the base plate material.
Request pricing & lead time
Submit dimensions for a documented quote
Upload drawings or STEP files with the required material grade and any supplementary test demands. Receive pricing, current stock status and the exact certificate package within one working day.
Shipments to Dammam, Musaffah or Ras Laffan can be arranged DDP with SABER/SCOC documentation included.