
Precision finishing for critical components
Precision Grinding & EDM
When a sealing face, bore or intricate profile cannot tolerate burrs or distortion, PartsMake delivers precision grinding and EDM for demanding industrial applications across the GCC. Our finishing capabilities support hardened steels, hard alloys and complex features where close fits and dependable geometry matter.
Built for demanding fits
-
01
Micron-level finishing
Grinding tolerances down to ±0.002 mm on specified cylindrical work.
-
02
Hard-to-machine geometry
Wire and sinker EDM for hardened materials, narrow slots and deep cavities.
-
03
Documented inspection
CMM inspection data books and material traceability available for qualifying orders.
Finishing capabilities
Precision where conventional cutting reaches its limits
Select the finishing process to suit the material, geometry and functional surface. Our grinding and EDM operations are designed for critical interfaces that need controlled dimensions and clean, consistent features.
01 / Form and flatness
Precision surface grinding
Large reciprocating-table grinding for flat faces, parallel surfaces and controlled finishing on hardened components, tool steel and precision mould bases.
- Dimensional precision
- ±0.003 mm
- Surface finish
- Down to Ra 0.2 μm
Typical work: valve plates, shear blades, mould base plates and precision sealing faces.
02 / Roundness and fit
CNC cylindrical grinding
Universal OD and ID grinding for multi-step diameters, shoulder features and close-fitting dynamic interfaces where concentricity and roundness are essential.
- Dimensional precision
- ±0.002 mm
- Roundness
- Down to 0.001 mm
Typical work: high-pressure pump plungers, turbine shafts and hydraulic actuator rods.
03 / Intricate profiles
Slow-wire EDM
Submerged slow-feeding wire EDM produces accurate profiles and narrow features in hardened steel and conductive hard materials, including work that is difficult to machine conventionally.
- Work envelope
- 600 × 400 × 350 mm
- Dimensional precision
- ±0.002 mm
Typical work: valve gates, spline keyways and subsea connector slots. Taper angles up to ±30°.
04 / Cavities and fine detail
Sinker EDM
Die-sinking EDM forms deep cavities, intricate ribs and internal features in hardened or refractory alloys without conventional tool pressure on delicate geometry.
- Work envelope
- 800 × 600 × 450 mm
- Dimensional precision
- ±0.005 mm
Specialty features: micro-hole drilling from Ø0.2 mm and deep blind cavities in Inconel 718.
Made for unforgiving service
No room for burrs, distortion or uncertain fits
High-pressure assemblies and precision tooling depend on the details that are difficult to see: a clean slot, a true cylindrical surface, or a flat sealing interface. PartsMake supports these requirements with process selection and inspection aligned to the part’s function.
High-pressure equipment
Pump cores and plungers
Ground diameters and controlled roundness for close-fit high-pressure pump components and hydraulic assemblies.
Tooling and moulds
Precision mould inserts
EDM profiles and ground faces for hardened inserts, fine details and cavities with demanding geometry.
Sealing interfaces
Deep-bore mating faces
Finishing for critical sealing surfaces where fit, surface condition and dimensional control support reliable assembly.
Hardened materials
HRC 60+ applications
Grinding and EDM processes suited to hardened steels, carbide and other hard-to-machine conductive materials, subject to drawing review.
Inspection and traceability
Verify the part, not just the process
Critical components can be supplied with the inspection and material records required for demanding industrial procurement and end-user review.
Dimensional verification
Temperature-stabilised CMM inspection suites at 20°C ±0.5°C, with certified dimensional inspection data books available for qualifying orders.
Material identity
PMI using XRF/OES spectrometry and EN 10204 3.1 material certification linked to heat-lot traceability.
Additional testing
Where specified, in-house NDT includes PT, MT and UT, with hydrostatic pressure testing available up to 20,000 PSI (1,380 bar).
Start with the drawing and fit
Need a critical surface or intricate feature finished?
Share the component drawing, material, hardness and inspection requirements. PartsMake can review the geometry and recommend a suitable grinding or EDM route for your application.
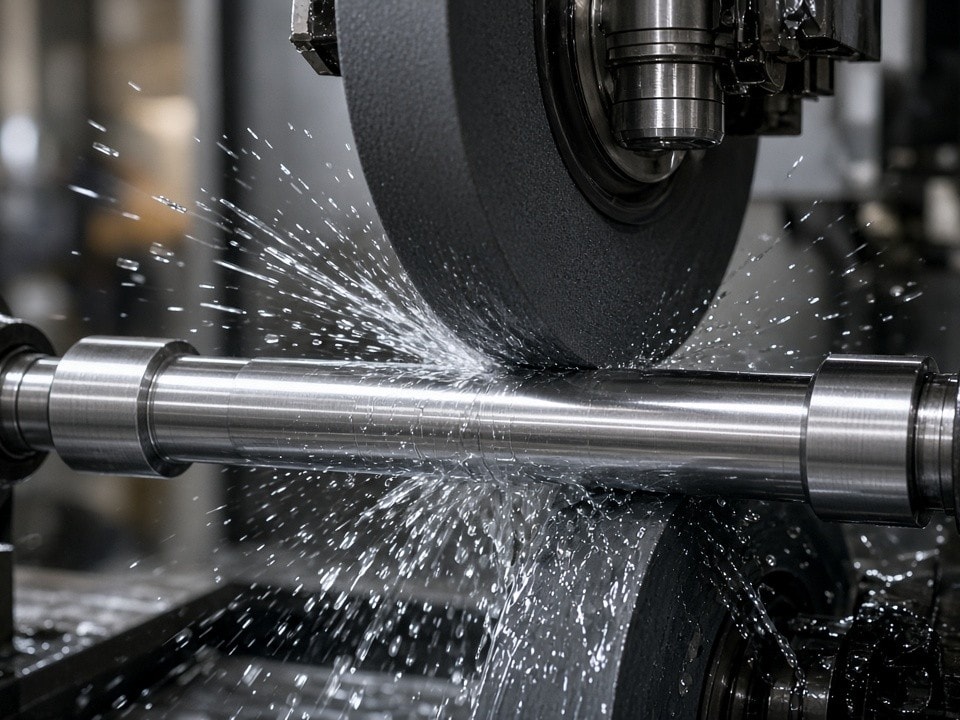
Cylindrical & Surface Grinding Services for Precision Industrial Parts | PartsMake
Precision cylindrical and surface grinding for shafts, sleeves and valve parts. Achieve Ra 0.1 µm cylindrical finishes, tight geometry and GCC-ready inspection records.
View details →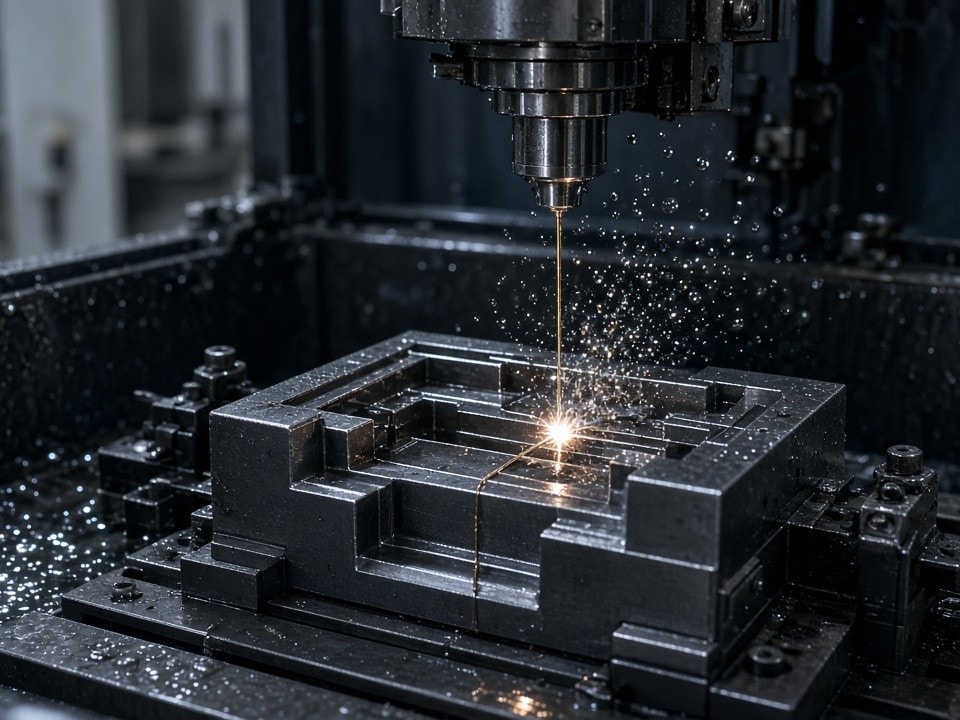
Wire EDM & Die Sinking for Hardened Alloys and Micro-Features in GCC Oil & Gas
Slow-feeding Wire EDM and CNC die-sinking services for Inconel, carbide and super-duplex parts. Micro-holes, shaped blind cavities and spline slots delivered with full material traceability to Dammam, Jubail and JAFZA.
View details →