
API 6D machining for GCC oil and gas
Valve Bodies & Flow Control Parts
Pressure-retaining bodies, sealing ball spheres and precision valve stems for ball, gate and choke valves across Middle East pipelines and refineries. PartsMake machines critical components to API 6D requirements, with documented material traceability and dimensional records.
For demanding pressure, sealing and flow-control applications in the GCC.
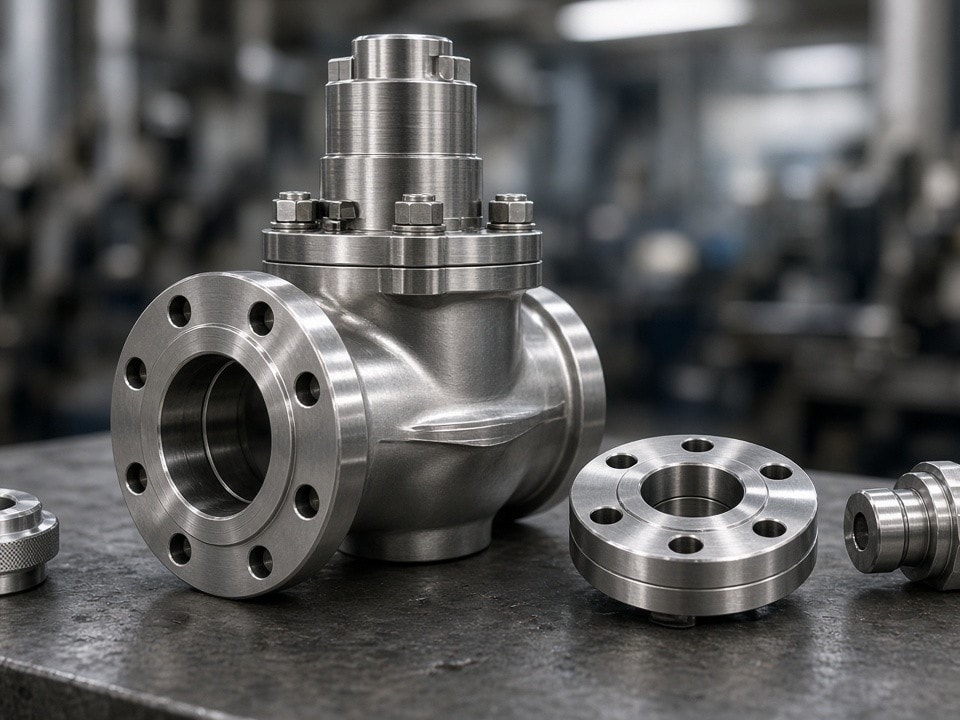
Precision where it matters
High-pressure sealing geometry, controlled surface finish and verified dimensions, supported by material records.
0.005 mm
Ball sphere roundness target
Ra 0.1–0.2 µm
Sealing-band finish capability
±0.02 mm
Typical valve-body bore tolerance
20,000 psi
Hydrostatic testing available
Machined components
Built around pressure, sealing and flow control
Each part is machined to its operating demands, from pressure-retaining body geometry to the fine finish and alignment required at sealing and stem interfaces.
01 / Pressure boundary
Pressure-retaining valve bodies
Forged or cast billets in 316L, Super Duplex 2507 and Inconel 718 are machined for consistent wall thickness and bore geometry under cyclic pressure.
- Typical envelope up to 850 mm diameter × 2,200 mm length
- Bore tolerances held to ±0.02 mm before final grinding
- 5-axis machining available for internal flow passages
02 / Sealing interface
Ball spheres and sealing bands
Slow-feed wire EDM followed by CNC cylindrical grinding produces sealing spheres up to 400 mm diameter for high differential-pressure service.
- Roundness below 0.005 mm
- Mirror grinding to Ra 0.1–0.2 µm on sealing bands
- Form measurement and surface profilometry for verification
03 / Actuation and load
Duplex and Hastelloy valve stems
Precision turning supports coaxiality and torsional strength in demanding stem applications, including duplex and Hastelloy grades.
- Coaxiality within 0.01 mm over lengths above 1,000 mm
- OD turning, keyway milling and thread rolling in one setup
- CMM reports verify runout and thread pitch diameter
Process selection
Match the route to the part
Choose a component to view a practical machining route based on material, geometry and service requirements.
Ball spheres above 200 mm diameter
Rough turning, then cylindrical grinding
Use cylindrical grinding after rough turning to achieve sealing-band Ra ≤ 0.2 µm. Verify sphere form and surface finish using form measurement and profilometry.
Hastelloy C276 stems requiring torsional strength
9-axis mill-turn with integrated thread rolling
Complete turning, keyway milling and threading in one setup to support alignment and mechanical performance. CMM reports confirm runout and thread pitch diameter against the drawing.
Super Duplex bodies for chloride service
Machine flow passages, then hone the bore
Use 5-axis milling for internal flow passages followed by bore honing. Maintain traceability to the material heat and inspect critical dimensions in a temperature-controlled CMM suite.
Quality and traceability
Inspection records from feedstock to final release
Material verification and documented inspection support API 6D component requirements, including sour-service traceability where specified.
Material verification
EN 10204 3.1 certificates are linked to heat numbers. PMI is carried out on every batch before it enters the shop floor.
Dimensional and surface inspection
Temperature-controlled CMM suites record critical dimensions on every part. Form measurement and surface profilometry verify ball sealing geometry and finish.
Testing and service conditions
Hydrostatic testing to 20,000 psi is available for completed assemblies. Salt-spray exposure testing can confirm external coating performance in coastal or desert conditions.
Regional project fit
Support for contractors and MRO teams across the GCC
Eastern Province MRO shops and JAFZA skid packagers can source replacement trim sets in small batches, with full data books and shorter lead times than the 24–40 weeks typical of overseas OEM routes.
Free-zone logistics support direct DDP delivery to Dammam, Musaffah and Ras Laffan yards. Site visits can be arranged at for ongoing programmes.
Tell us your valve type, material and delivery location.
Discuss your projectRequest for quotation
Share your drawing or part number
Include the material grade, pressure rating and required certifications. For most valve components, preliminary lead times and pricing are issued within two working days.
For ongoing programmes, contact us to arrange a site visit at or email info@partsmake.ae.