
GCC mining & heavy equipment
High-Load Bushings & Pivot Pins
PartsMake manufactures oversized, precision-machined articulation pins and self-lubricating alloy bushings for open-pit excavators, heavy dump trucks and large bulldozers operating in demanding desert conditions.
Designed to address abrasive silica sand, impact loading and thermal cycling, our components help reduce pin seizure, breakage and abnormal wear across critical joints.
±0.002 mm
CNC-ground pin tolerances
Ra 0.2–0.4 μm
Sliding-surface finish
24 hours
DFM feedback target
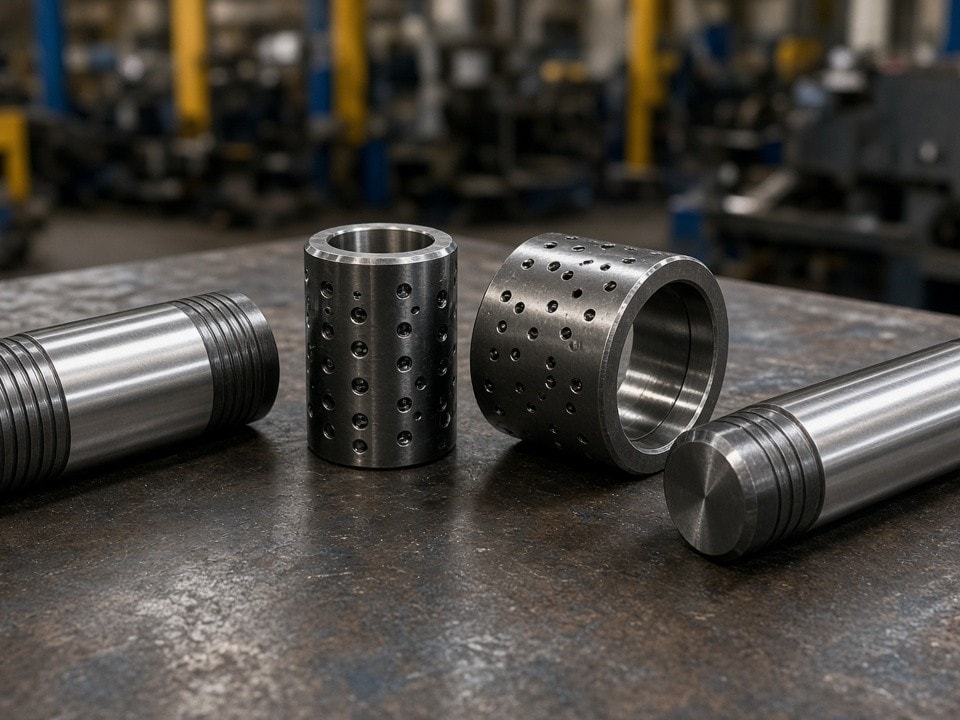
Made for abrasive, high-impact duty
Material selection, heat treatment and oil-retention geometry are specified around the working conditions of GCC mining and earthmoving fleets.
Engineering for desert mining
Help protect critical joints from sand, shock and heat.
Airborne silica can work into clearances, compromise lubrication and accelerate wear. Combined with heavy loads and thermal cycling, these conditions can contribute to bushing walk, pin seizure and premature joint failure.
PartsMake engineers oversized pivot pins and high-load bushings around these operating challenges. Controlled heat treatment, accurate fitment and carefully machined lubrication paths help limit dry-running friction and the sand-grinding effect on mating surfaces.
Abrasive silica
Internal geometries support grease distribution and particle flushing.
Oscillating loads
Surface hardening helps resist deformation under repeated articulation.
Remote maintenance
Replacement manufacturing and GCC delivery options support field repairs.
Component engineering
Two components, engineered to work together.
Pin and bushing performance depends on material, surface condition, fit and lubrication working as a system. Specify individual parts or request a review of the joint assembly.
01 / Pivot pins
High-load alloy steel pins
Heavy-duty pins are produced from 42CrMo and 40CrNiMo alloy steels, selected for fatigue strength and impact resistance in demanding articulation points.
- —Quenching and tempering: controlled processing to establish the required core-to-surface hardness balance.
- —Case and surface hardening: deep-case carburising and induction surface hardening options help withstand oscillating loads.
- —Precision fitment: CNC grinding to tolerances within ±0.002 mm helps reduce looseness and vibration-induced fatigue.
02 / Bushings
Self-lubricating alloy bushings
Designed for high-pressure, low-speed applications where dust can compromise conventional lubrication. Options include high-strength bronze alloys and hardened steel.
- —Deep-hole oil-retention spiral grooves: precision-turned channels in the bore help capture grease and distribute it across the contact surface.
- —Oil and grease pathways: deep-bore oil-storage and drainage geometry supports lubricant movement through the joint.
- —Debris management: internal geometry helps flush silica particles and reduce scoring of mating pins.
Surface finish
Ra 0.2–0.4 μm
Specified on sliding surfaces to help minimise friction.
Dimensional control
±0.002 mm
CNC-ground pin tolerances for accurate fitment.
Engineering response
Within 24 hours
Target timeframe for DFM feedback on submitted requirements.
Quality & verification
Documented checks from material to finished component.
Each component batch is supplied with a data book to support the maintenance and quality requirements of regional energy majors and heavy industrial operators.
Material traceability
EN 10204 3.1 material certificates for alloy steel and bronze stock.
Metrology
100% CMM inspection for geometric tolerances and roundness.
Non-destructive testing
Level II certified Dye Penetrant (PT) and Ultrasonic (UT) testing to check for sub-surface cracks and forging defects.
Dimensional stability
Post-machining stress relief helps components maintain stability under high hydraulic forces.
Surface protection
Specialised surface treatments can help resist oxidation in high-salinity coastal mining regions.
Supply & field support
Support for urgent maintenance requirements across the GCC.
Equipment off-road status can carry significant cost. PartsMake connects international manufacturing with delivery options for remote mining and construction sites.
01
DDP delivery
Door-to-site shipping across the GCC, including customs clearance and SABER/SASO documentation support.
02
Urgent production
Dedicated production lines for urgent replacement parts, intended to help avoid typical six-month global OEM lead times.
03
Regional dispatch
Bonded hub access supports dispatch from regional free zones to remote operating sites.
Common questions
Planning a replacement or joint review?
Share your drawings, component measurements or damaged-part details to help our engineering team assess the requirement.
What should I send for a technical review?
Submit drawings or damaged-component specifications. Include material, operating conditions and joint details where available. DFM feedback is targeted within 24 hours.
Which materials and hardening processes are available?
Pivot pins can be manufactured from 42CrMo and 40CrNiMo, with controlled quenching and tempering, deep-case carburising and induction surface hardening options.
Can you supply inspection and material documentation?
Batch documentation can include EN 10204 3.1 material certificates, 100% CMM inspection, and Level II certified PT and UT test results.
Request a quotation
Send your drawing or damaged component details.
Request a technical review of your high-load pivot pin or bushing. Our engineering team can provide DFM feedback to assess fit, wear characteristics and suitability against standard off-the-shelf replacements.
Email: info@partsmake.ae
Facility:
Share your requirements
For a faster review, include part dimensions, material requirements, equipment model and the application environment.