
Precision EDM for flow-control components
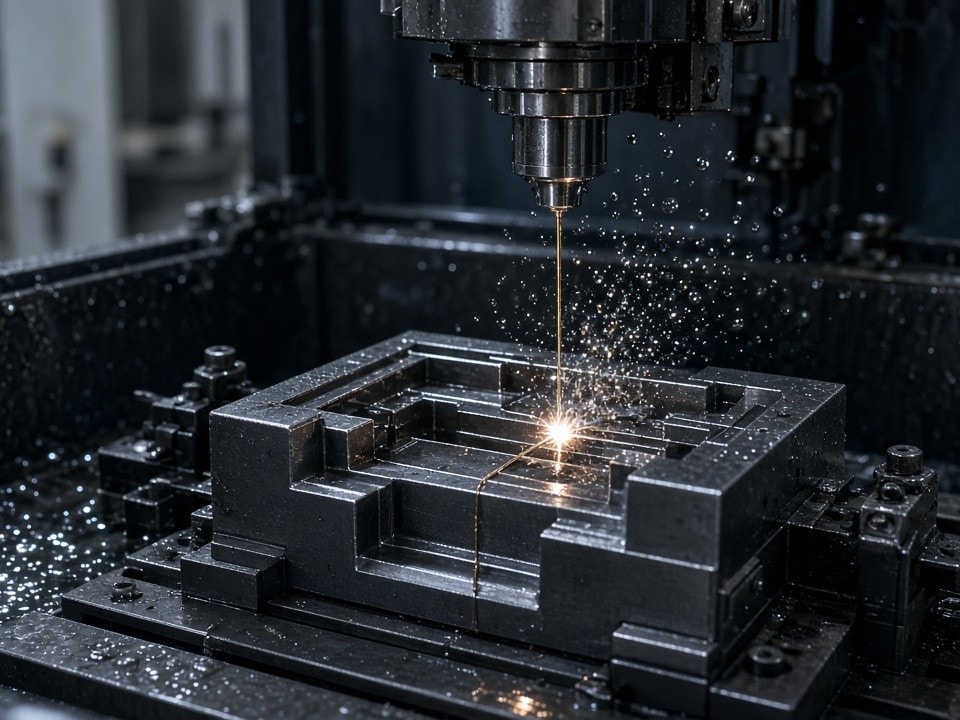
Wire EDM & Die Sinking for Hardened Components
PartsMake provides submerged slow-feeding Wire EDM and CNC die-sinking for demanding valve and nozzle work across the Eastern Province and UAE. Cut complex features in already-quenched alloys and tungsten carbide without a heat-affected zone.
From shaped blind holes in oil and gas sampling valves to micro-orifices and spline slots, spark erosion helps avoid the broken tools and distortion associated with milling hard or deep, narrow features.
- ±0.002 mm Wire EDM position tolerance
- 100% CMM verification
- 7–12 working-day first articles
Wire EDM finish
0.18 µm Ra
Die-sinking tolerance
Down to ±0.005 mm
Machine envelope
Accuracy built around demanding features
Submerged cutting and controlled EDM parameters support intricate geometries in quenched Inconel 718, 17-4PH, Super Duplex 2507 and tungsten carbide.
Inspection and certification
Every part receives 100% CMM verification at 20 °C ±0.5 °C, with EN 10204 3.1 certificates and full inspection data books.
01 · Wire EDM
Slow-feeding, submerged 4-axis cutting
- Working envelope
- 600 × 400 × 350 mm
- Wire diameter
- 0.10–0.30 mm
- Taper capability
- Up to ±30°
- Position tolerance
- ±0.002 mm
0.18 µm Ra on valve gates and spline keyways.
02 · Die-sinking EDM
CNC cavities, ribs and micro-holes
- Working envelope
- 800 × 600 × 450 mm
- Machine capability
- C-axis sinkers
- Minimum electrode diameter
- 0.2 mm
- Feature tolerance
- Down to ±0.005 mm
For deep ribs, shaped blind holes and intricate micro-hole work.
Typical GCC applications
Complex features in hard-to-machine parts
EDM makes internal geometries and fine details practical after heat treatment, where conventional cutting tools can deflect, break or leave delicate sections distorted.
Oil & gas · Sampling valves
Shaped blind holes and undercut galleries
Sinker electrodes form internal cavities directly in hardened valve trim—features that milling tools cannot reach reliably without deflection or breakage.
Desalination & chemical injection
Carbide spray nozzles
Produce arrays of 0.2–0.8 mm orifices with consistent geometry and no recast layer.
Downhole equipment
Long spline slots
Finish mandrel and drill-collar spline slots by Wire EDM after rough turning, avoiding tool wander in high-nickel alloys.
Choosing the right route
Match the process to the feature
Select a process based on material hardness, section thickness, feature access and production volume.
Choose Wire EDM for slots, profiles and keyways
A strong fit for parts already heat-treated above 45 HRC, thin walls below 3 mm and features with aspect ratios above 10:1. Spark erosion helps preserve flatness and roundness while avoiding burrs and tool wander.
Choose die-sinking for inaccessible cavities
Use shaped electrodes for internal blind holes, undercut galleries, deep ribs and micro-holes in hardened material where a rotating cutter cannot safely reach.
Consider a hybrid route for higher volumes
For volumes above 50 identical pieces, we evaluate combining 5-axis milling for bulk material removal with EDM for the final micro-features.
Regional readiness
Documentation and logistics for GCC operators
Every shipment includes PMI reports and CMM point-cloud data. NDT records are available on request.
Delivery terms
DDP to Dammam, Jubail, Musaffah or JAFZA
Clearance
SABER/SASO processed
First-article lead time
7–12 working days after drawing approval for micro-hole or shaped-cavity work
Request a quote
Send your drawing or STEP file
Share your part requirements for DFM notes and a fixed quotation within one business day. For enquiries by email, contact info@partsmake.ae.