
Hydraulic components for demanding MRO work
Heavy Duty Hydraulic Cylinders & Rods for Port Cranes & Loaders
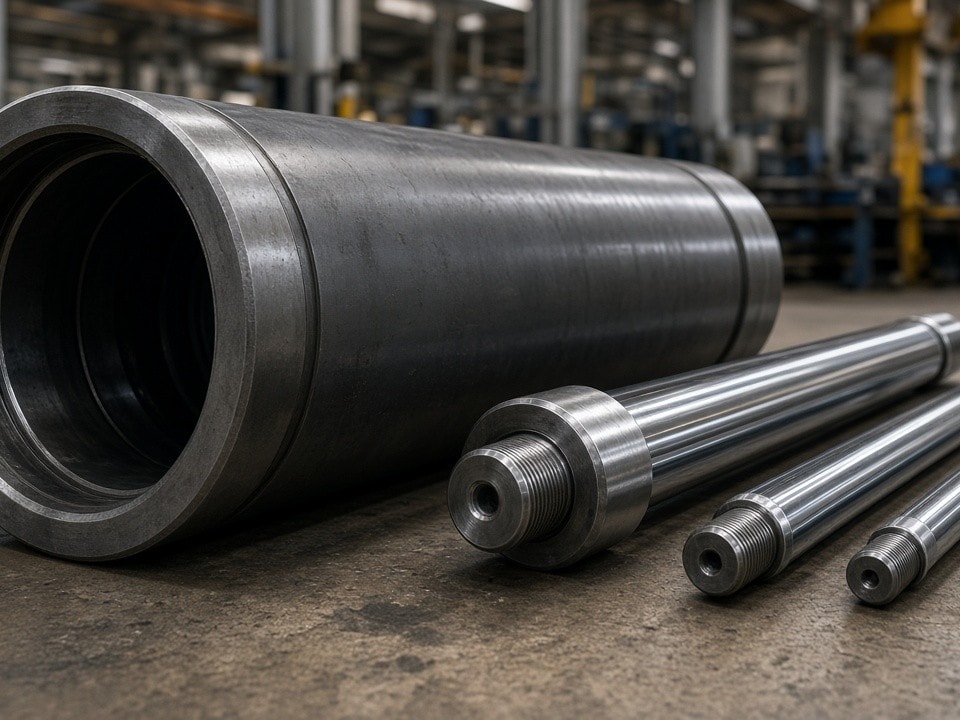
PartsMake supplies large-tonnage cylinder barrels, pistons and precision piston rods to Tier-2 and Tier-3 MRO contractors across Saudi Arabia and the UAE. Built for continuous outdoor exposure and hydraulic oil temperatures that regularly exceed 80 °C.
0.005 mm
Maximum cylindricity over the bore
Ra 0.2 µm
Final barrel surface finish
350 bar
Full-stroke test rig pressure
The failure pattern
High ambient heat can turn bore damage into downtime
In Middle East outdoor operation, hydraulic oil temperatures can climb beyond 80 °C. Standard seamless cold-drawn tubes may develop scoring inside the bore as operating conditions intensify. That surface damage accelerates seal wear and can lead to leakage within weeks.
A controlled finish from the bore out
After initial boring, deep-hole honing removes the stressed layer left by tube drawing and restores a consistent cylindrical form. The result is a carefully measured bore surface designed to support reliable sealing in demanding service.
Cylinder barrel process
Deep-hole honing for large-bore accuracy
PartsMake processes seamless cold-drawn steel tubes from 180 mm to 450 mm inside diameter, with honing capacity for lengths up to 3,200 mm.
01 / Machining sequence
From tube preparation to final bore
- 01Seamless cold-drawn tube preparation, followed by gun drilling and rough boring.
- 02Multi-pass deep-hole honing to bring cylindricity within 0.005 mm.
- 03Final finish to Ra 0.2 µm, checked along the full length using a skidless profilometer scan.
02 / Inspection and traceability
Measured, documented and tied to the material heat
- EN 10204 3.1 mill certificate linked to the heat number.
- CMM report covering bore diameter and straightness.
- Full-length surface-finish scan recorded for the barrel.
Piston rod production
A ground and plated rod with seal protection in mind
Rods are produced from induction-hardened 42CrMo4 or 38MnVS6 bar stock, with the finished surface prepared for demanding cylinder service.
Precision grinding
±0.01 mm
Diameter tolerance after cylindrical grinding.
Hard-chrome plating
25–35 µm
Electroplated chrome thickness for corrosion protection.
Superfinished surface
Ra 0.1 µm
Post-plate finish to remove edge build-up that could cut seals.
Chrome thickness verification
Every rod is checked by X-ray fluorescence at three axial locations, providing a defined inspection record for the plated surface.
Material options
Additional corrosion resistance for coastal and sour-gas sites
For equipment operating near desalination plants or in Jubail industrial zones, specify Super Duplex 2507 barrels paired with an Inconel 625 overlay on the rod seal area to provide additional resistance to chloride pitting.
Barrel option
Super Duplex 2507
Rod seal-area option
Inconel 625 overlay
Plating lines maintain bath chemistry and current-density records, supporting traceability back to each batch.
Built around real equipment
Fitment for port cranes and heavy wheel loaders
Components are configured for large-scale lifting and loading applications, with end features machined to suit the assembly.
Reach-stackers
250 mm bore
Typical lift-cylinder configuration for port handling equipment.
Quay cranes
320 mm bore
Typical luffing-cylinder configuration for crane applications.
Rod-end machining
Integrated fitment
Spherical bearings or clevis ends can be machined in the same mill-turn cell to maintain concentricity.
1,000
full-stroke cycles
Skid-mounted test before shipment
Facility test rigs run 1,000 full-stroke cycles at 350 bar before components are shipped.
Documentation and delivery
A data book for every cylinder
Each cylinder is supplied with records covering the material, machining, coating and pressure testing stages.
- Material certificates
- Honing charts
- Chrome thickness readings
- Hydrostatic test records at 1.5× working pressure
Regional delivery for UAE and Gulf yards
DDP terms cover clearance through JAFZA or Dammam, with final delivery to yards in Musaffah, Yanbu or Ras Laffan within 10–15 working days.
Technical questions
Before you request a quotation
What information should I send for a quotation?
Share the bore diameter, stroke length, working pressure and rod-end configuration so the team can review your cylinder requirements.
What inspection records are supplied?
The data book includes material certificates, honing charts, chrome thickness readings and hydrostatic test records at 1.5× working pressure.
Can the team review an existing cylinder failure?
Site visits to review existing cylinder failures can be arranged from the facility.
Request cylinder specifications
Get engineering feedback and a fixed quotation
Send your bore diameter, stroke length, working pressure and rod-end configuration. Engineering feedback and a fixed quotation are returned within one working day.
Site visits to review existing cylinder failures can be arranged from the facility.
Email info@partsmake.aeSend your requirements
Include any available drawings or existing component details with your enquiry.