
Industrial finishing · Outdoor duty
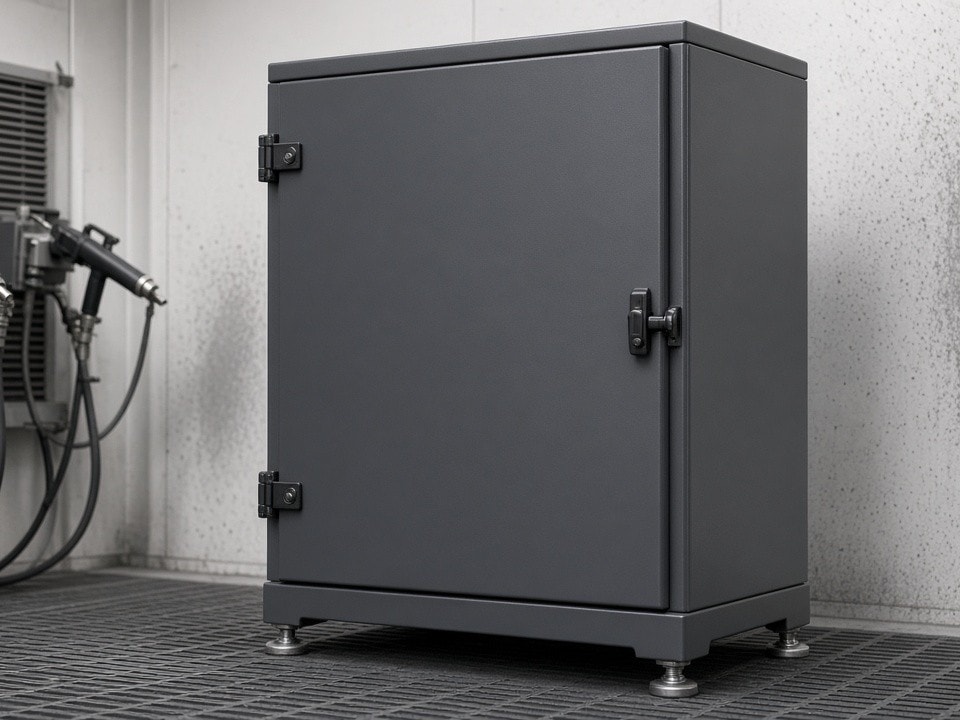
Industrial Epoxy & Powder Coating for Outdoor Control Cabinets
PartsMake applies high-build epoxy and UV-stabilised polyester powder coatings to large steel and aluminium enclosures built for direct Gulf sunlight and surface temperatures reaching 60 °C.
Designed to resist yellowing, chalking and thermal-shock cracking, these coating systems help protect outdoor control cabinets, switchgear housings and skid-mounted electrical panels through demanding coastal and desert conditions.
60 °C
Surface-temperature duty
2,000 h
Salt-spray test duration
6,000 mm
Maximum component length
Coating specification
A two-layer system matched to regional conditions
Choose the coating layer details below. Both systems are applied after abrasive preparation to Sa 2.5 and cured at a metal temperature of 200 °C.
Corrosion barrier · Carbon steel
High-build epoxy primer
A 60–80 µm primer layer provides the corrosion-resistant foundation for fabricated steel cabinets and electrical housings.
UV-stabilised · Outdoor finish
Polyester topcoat
An 80–120 µm UV-stabilised polyester topcoat is specified to maintain colour and gloss under continuous solar radiation, while helping resist yellowing and powdering.
Repeatable production process
Prepared, applied and checked
Parts up to 6,000 × 2,500 mm are abrasive-prepared to Sa 2.5, electrostatically coated and cured in forced-air ovens at 200 °C metal temperature. Calibrated gauges verify film thickness at multiple points, with average total DFT recorded on every job card.
Batch-level verification
Measured performance, supplied with the job
Each production batch includes documented test results alongside material certificates and dimensional reports. Cross-cut adhesion and film-thickness measurements are included in the inspection package.
| Test | Standard / exposure | Recorded result |
|---|---|---|
| Cross-cut adhesion | ISO 2409 | Class 0 or 1 on prepared surfaces |
| Salt-spray resistance | ASTM B117 · 2,000 h | No blistering or under-film corrosion |
| Thermal shock | 50 cycles · –20 °C to +80 °C | No cracking or delamination |
| Gloss retention | 2,000 h QUV exposure | At least 85% of original value |
Film thickness is measured at multiple points with calibrated gauges; average total DFT is recorded for each job.
Fabrication to finished assembly
Coating integrated with sheet-metal and welding work
Finishing follows laser cutting, press-brake forming and certified welding. Weld seams receive additional stripe coating to maintain uniform coverage.
Cabinets can be supplied assembled with doors, hinges and mounting plates already coated, or as flat-pack kits for site assembly. Neutral packaging and laser-etched part numbers are available for free-zone stockists.
A practical fit for outdoor enclosures
- Suitable for cabinets in coastal or desert locations, including applications that require documented adhesion and thickness records.
- A considered choice for enclosures housing electronics that cannot tolerate surface degradation.
- Not intended for immersion service or parts subject to repeated mechanical impact.
Request for quotation
Share your cabinet requirements
Send drawing files or cabinet dimensions, required material grade, target film thickness and colour reference. Typical lead time for coated assemblies is 12–18 working days from approved drawings.
Direct DDP delivery is available to Dammam, Musaffah or JAFZA.
Send an enquiry
Include any inspection, colour or packaging requirements with your request.