
Compression-moulded seals for GCC sour service
Elastomer & Seal Molding for High-Temperature Sour Gas Service in the GCC
Specify oil- and heat-resistant FKM, HNBR and FFKM seals for demanding wellhead, process and desalination applications. PartsMake focuses on sealing force that lasts through thermal cycling, pressure spikes and exposure to H₂S-rich fluids.
Designed for the realities of Gulf service: ambient temperatures above 50 °C, heavy oils and sour gas that can accelerate hardening, cracking and seal leakage in the wrong compound.
Below 12%
Compression set target after 70 hours at 200 °C
10–15 days
Typical first-article lead time after drawing approval
Moulding capacity
100–300-tonne presses
Multi-cavity tooling for parts up to 300 mm diameter.
Gas tightness
High-pressure validation
Helium leak-rate testing below 1 × 10⁻⁶ atm·cc/s at 20,000 psi.
Batch control
Traceable production
Compound batch, cure data and compression-set results supplied with each project.
Built for regional conditions
Why standard seals fail in GCC service
High surface temperatures combined with hydrogen sulphide can make conventional nitrile and standard fluoroelastomer seals harden and crack prematurely. For operators, the result may be lost sealing force, leakage and unplanned shutdowns.
Field condition indicator
Over 40% compression set
Field data from Eastern Province wellheads and Yanbu desalination trains recorded compression set above 40% within six months when the wrong grade was selected. Compound choice and cure control are critical to maintaining sealing force.
Compound selection
FKM, HNBR and FFKM for demanding seal duty
Choose the elastomer around operating temperature, fluid exposure, movement and pressure. These compound families are held for immediate tooling trials.
Fluoroelastomer
FKM / Viton for hot oil and sour crude
FKM grades are rated for continuous service up to 200 °C, with a 15% volume-swell limit in sour crude at 150 °C. Specify the grade against the actual fluid composition and temperature profile.
Hydrogenated nitrile
HNBR for dynamic wellhead applications
HNBR compounds are available for dynamic service up to 160 °C and differential pressure up to 5,000 psi. They are suited to applications where movement and pressure cycling must be considered together.
Perfluoroelastomer
FFKM for steam and amine service
FFKM is available for demanding steam and amine applications where FKM may reach its service limits. Post-cure is carried out in nitrogen to help prevent surface oxidation.
Batch performance target
Compression set below 12% after 70 hours at 200 °C, tested to ASTM D395 Method B. Helium leak rates below 1 × 10⁻⁶ atm·cc/s at 20,000 psi.
Process and equipment
Compression moulding controlled from cure to inspection
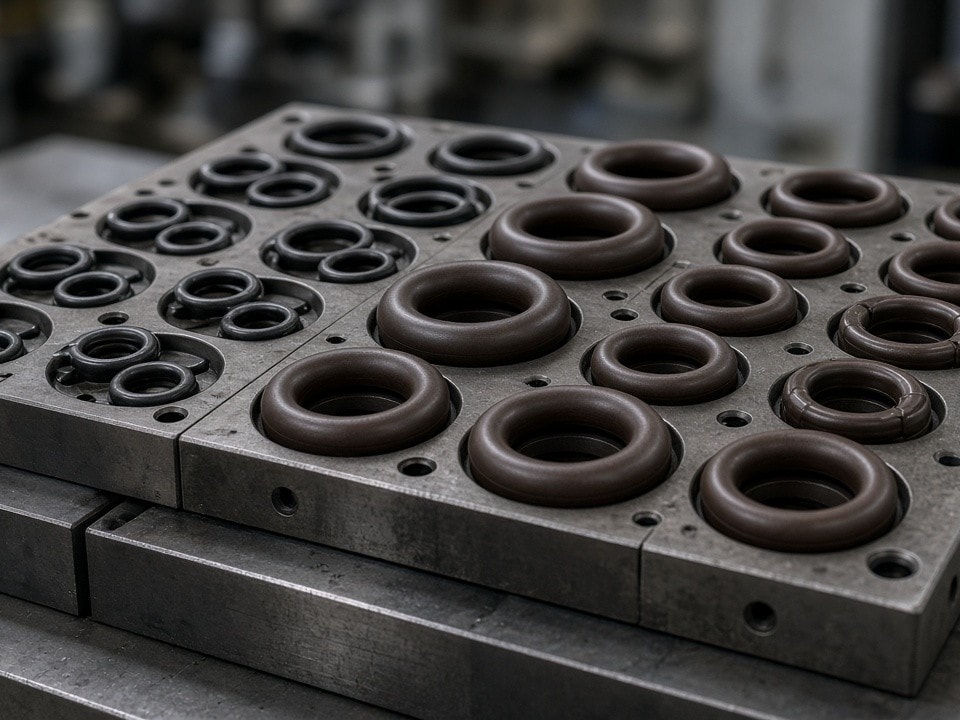
Cure cycles are validated with moving-die rheometers for each compound lot. Nitrogen post-cure ovens are used for FFKM parts, followed by 100% visual inspection and batch sampling for hardness, tensile strength and compression set.
From approved drawing to first articles
Typical lead time is 10–15 working days. Maximum part weight depends on cavity volume rather than press tonnage, supporting large cross-section O-rings and custom packer elements beyond typical injection-moulding limits.
Tooling and geometry range
Prototype tooling
In-house machined aluminium tools for quantities of 50–500 pieces.
Production tooling
P20 or H13 steel tools with flash-free parting lines.
Custom part features
Non-circular cross-sections, integrated lips and bonded metal inserts without secondary bonding operations.
Section dimensions
Minimum cross-section thickness from 1.5 mm; maximum wall thickness up to 25 mm for heavy packer elements.
Regional applications
Seal sets for contractors across the Gulf
Parts are specified to the service conditions and supplied with a material traceability package, including compound batch number, cure data and compression-set results.
Wellhead valves
Stem packing and bonnet seals
Replacement sets for 6,000–15,000 psi gate valves in Dammam and Jubail.
Pumping systems
Backup rings and V-packing
Custom sets for progressive cavity pumps handling produced water with high chloride content.
Desalination
Large-diameter flange gaskets
Gaskets for SWRO high-pressure manifolds in Abu Dhabi and Ras Laffan.
Downhole and workover
Wear pads and packer elements
Custom parts for workover operations in sour Khuff reservoirs.
Quality documentation
Traceable by batch and ready for review
Shipment records
Each shipment includes EN 10204 3.1 equivalent certificates for the elastomer compound, durometer readings and pressure-test records where specified.
Identification options
FTIR PMI is available on request for critical sour-service lots. Parts can be laser-marked with compound and date codes, or supplied in neutral packaging for trading-house customers.
Request a quote
Start with your drawing, sample or operating conditions
Send part drawings or existing sample dimensions together with operating temperature, pressure and fluid composition. A firm quotation with tooling cost and sample lead time is typically provided within 24 hours.
Local collection from the JAFZA bonded facility or direct DDP delivery to Dammam, Musaffah or Doha yards can be arranged.