
Industrial Welding & Cladding
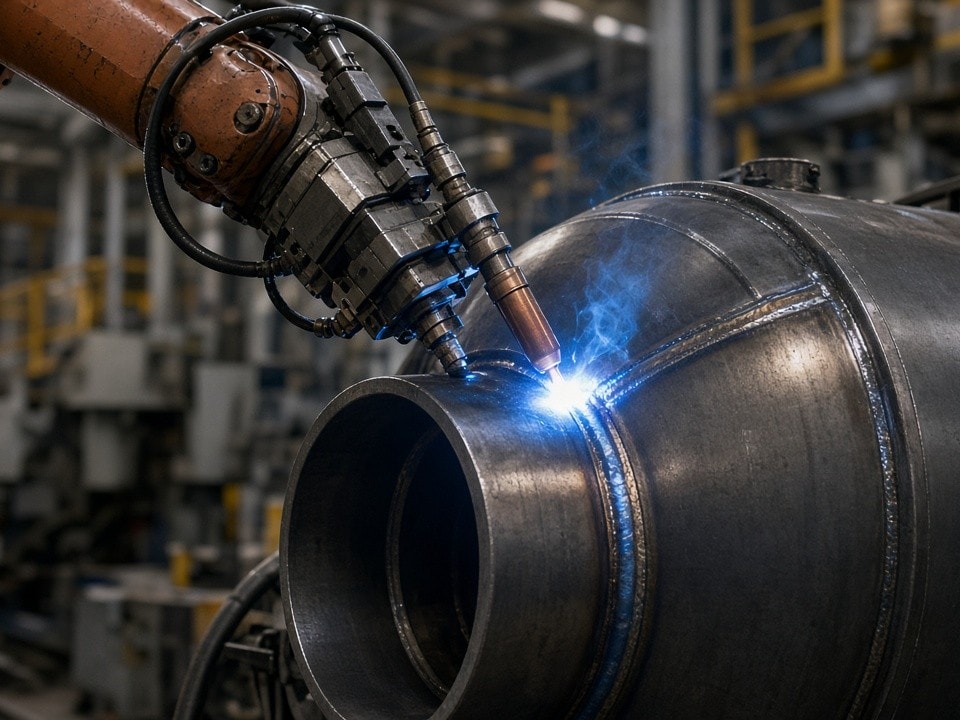
PartsMake delivers robotic TIG and submerged arc welding for pressure-rated weldments and corrosion-resistant overlays. Our certified specialists help Middle East oil and gas operators extend component life while reducing the cost of full superalloy construction.
10 t
Maximum workpiece capacity
3–8 mm
Typical overlay thickness
24 hrs
Drawing review target
Built for demanding service
Pressure-rated assemblies, valve bodies, wellhead spools, pipe fittings and manifold blocks for sour service and high-chloride environments.
Certified overlay capabilities
A bonded alloy barrier without a full alloy forging
Automatic TIG cladding applies Inconel 625 or 2507 duplex layers onto carbon steel substrates. The metallurgical bond protects against H₂S, chlorides and CO₂ while controlling material cost.
Performance-focused process control
Dilution is controlled below 5% to support corrosion performance equivalent to solid Inconel or duplex construction.
ASME and AWS qualified
All welders and procedures hold current ASME and AWS certification, including ASME Section IX and AWS D1.1/D1.6 qualifications.
Overlay materials
Automatic TIG deposition of Inconel 625 or 2507 duplex layers for valve bodies, wellhead spools and pipe fittings.
Inspection at every batch
Visual inspection, dye penetrant or magnetic particle testing, and ultrasonic examination where specified.
Traceable shipment records
Mill certificates and welding procedure qualification records travel with every shipment.
Equipment and process envelope
Capacity for new fabrication and urgent repair
These resources support legacy-component repair when full replacement lead times exceed the operational window.
Robotic TIG cells
500 A power sources with seam-tracking sensors.
Submerged arc stations
For structural skids and large-diameter flanges.
Wire inventory
In-house Inconel 625 and duplex wire for rapid scheduling.
10 t work envelope
Lifting and positioning fixtures for large assemblies.
Testing capability
Post-weld heat treatment and hydrotest up to 20,000 psi.
Cost and schedule advantage
Use a carbon steel base where a thin alloy layer does the work
For sour service or high-chloride seawater, cladding can deliver the required corrosion resistance without the procurement burden of solid Inconel or duplex forgings.
35–55%
Potential material savings
Compared with solid Inconel or duplex forgings, while meeting NACE MR0175 / ISO 15156 requirements.
Common regional applications
Procurement teams in Dammam, Jubail and Musaffah commonly use cladding for valve trim, choke bodies and manifold blocks.
Engineering review within 24 hours
Our engineers flag geometry or thickness constraints that may affect overlay feasibility.
When another route may be better
Components with complex internal passages or frequent design iterations may be better suited to five-axis machining or additive routes. We assess the design before recommending the process.
Documentation and traceability
Complete records delivered with every order
Documentation is prepared for technical review, project close-out and direct delivery to Gulf-region sites.
EN 10204 3.1 material certificates for base metal and consumables
Welding procedure specifications and qualification records
Dimensional reports from calibrated CMM or laser scanning
NDT reports signed by Level II inspectors
SABER/SASO compliance files prepared for direct DDP delivery to site
Technical guidance
Questions teams ask before specifying cladding
Share your drawings or parts list and our technical sales team will help confirm the right overlay specification.
Next step
Send your drawings or parts list
Receive a fixed-price quotation, material lead time and recommended overlay specification within two business days. For urgent MRO requirements, contact the technical sales team on WhatsApp for a same-day review.
Email: info@partsmake.ae
Address:
WhatsApp: